


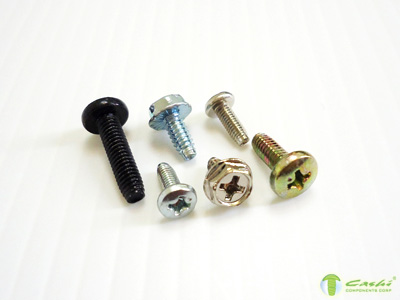
Special Triangular Thread Profile Helps Reduce Thread-Forming Resistance
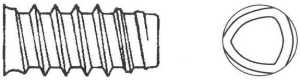
TYPE-TT does not use a completely circular thread cross-section. Instead, it adopts a triangular, trilobular, or similar profile. During installation, the raised portions of the thread gradually displace the wall of the pilot hole, reducing the resistance that would otherwise occur if the entire thread circumference contacted the workpiece at the same time.
Actual driving torque will still depend on workpiece material, hardness, pilot hole size, and screw surface condition.
Forms Internal Threads in Pre-Drilled Metal Holes
When driven into a properly sized pilot hole, the screw plastically deforms the metal around the hole and forms internal threads that match the screw profile. This can reduce the need for a separate tapping operation.
A properly sized pilot hole is generally still required. This screw is not designed to drill directly into every material or thickness.
Helps Reduce Metal Chip Generation
Compared with self-tapping screws that use cutting slots or cutting edges, TYPE-TT primarily forms internal threads by displacing material, helping reduce metal chips generated during the threading process.
This feature is useful for electronic equipment, mechanical components, enclosures, and precision assemblies where internal cleanliness is important.
Increases Thread Contact and Frictional Resistance
Because the workpiece threads are formed directly around the screw profile, good contact can be created between the screw threads and the formed internal threads. The special triangular profile can also increase localized contact pressure and frictional resistance, helping reduce the possibility of self-loosening under general vibration conditions.
Actual anti-loosening performance should still be confirmed according to applied load, vibration level, effective thread engagement, and tightening torque.
May Reduce the Need for Nuts
TYPE-TT screws can be driven directly into metal workpieces with suitable pilot holes. In some one-sided assembly applications or locations where installing a nut on the back side is difficult, this can reduce the need for nuts and other additional components, simplifying the assembly structure.
Simplifies Drilling and Tapping Processes
Once the pilot hole is prepared, the screw can form the internal thread and complete the fastening operation in a single process. This can reduce the need for pre-tapping with a tap and help simplify manufacturing steps and process management.
Improves Pull-Out and Fastening Stability
With an appropriate pilot hole size and effective thread engagement length, the screw threads can fully engage with the formed internal threads in the workpiece, providing stable pull-out resistance and clamping performance.
Actual load capacity should be verified according to workpiece material, thickness, thread diameter, pilot hole size, and installation depth.
Suitable for Automated Assembly
TYPE-TT screws with consistent specifications can be used with vibratory bowls, feeding tracks, and automatic screw-fastening equipment, making them suitable for high-volume production and assembly lines with demanding cycle-time requirements.
For automated fastening, rotational speed, downward force, thread-forming torque, and stopping position should be properly controlled to avoid cross-threading, thread stripping, or screw breakage.
Suitable for Various Metal Materials
Depending on product design, TYPE-TT screws can be used with thin steel sheet, aluminum alloys, zinc alloys, die-cast parts, and other metal workpieces. Because ductility, hardness, and wall thickness vary between materials, a suitable thread profile, screw hardness, and pilot hole diameter should be selected for each application.
Multiple Head Types and Drive Options Available
Pan heads, countersunk heads, hex heads, flange heads, and other head styles can be selected according to product appearance, installation space, tooling, and fastening requirements. Drive options can include Phillips, Torx, hex socket, external hex, and others.
Customization Based on Drawings and Samples
TYPE-TT screws can be customized according to customer engineering drawings or physical samples, including screw head type, drive style, triangular-thread profile, thread diameter, thread pitch, length, point configuration, material, hardness, tolerances, heat treatment, and surface treatment.
Common Applications
TYPE-TT screws are commonly used in:
- Metal enclosures, cabinets, and sheet metal structures
- Electronic and electrical equipment
- Automotive and motorcycle components
- Aluminum alloy and zinc alloy die-cast parts
- Home appliances and consumer products
- Telecommunications and information equipment
- Motors, fans, and mechanical components
- Instruments and precision equipment
- Metal furniture and hardware accessories
- One-sided assembly locations or areas where rear-side nut installation is difficult
- Mass-production and automated fastening lines
Key Considerations When Selecting TYPE-TT
Before selection, confirm the workpiece material, material hardness, sheet thickness, pilot hole size, effective thread engagement length, and expected load. The workpiece must have sufficient plasticity and ductility to form a complete internal thread during the thread-forming process.
Pilot hole size is one of the most important factors affecting fastening quality. If the pilot hole is too small, thread-forming torque may become excessively high, potentially causing screw breakage, drive recess damage, workpiece cracking, or excessive load on the fastening equipment. If the pilot hole is too large, thread engagement may be insufficient, resulting in free spinning, thread stripping, or reduced pull-out strength.
The screw should be harder than the workpiece material to reliably form the internal thread, while still maintaining sufficient core toughness. If the surface hardness is too high and core toughness is insufficient, there may be a risk of brittle fracture during installation.
Appropriate rotational speed, downward force, thread-forming torque, and final tightening torque should be set during fastening. The torque required during the thread-forming stage differs from the final clamping torque after the joint is seated. Incorrect shut-off torque may result in insufficient fastening or damage to the formed internal threads.
TYPE-TT screws may be removable depending on product design, but repeated assembly and disassembly can wear or deform the formed internal threads and reduce friction during subsequent installations. If frequent maintenance or repeated disassembly is required, the expected service life of the formed threads should be evaluated, or alternative structures such as nuts, insert nuts, or pre-tapped holes should be considered.
For applications involving severe vibration, high loads, outdoor exposure, humidity, or corrosive environments, anti-loosening methods, screw material, surface treatment, and the risk of galvanic corrosion between dissimilar metals should also be evaluated.


