


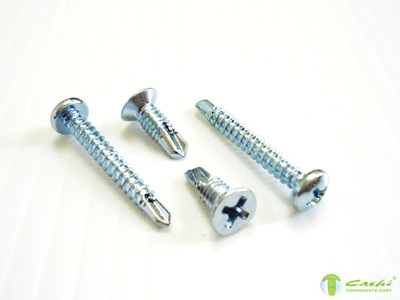
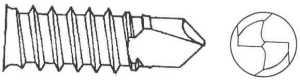
Integrates Drilling, Tapping, and Fastening
The drill point at the tip of a DRILL TAPPING screw first penetrates the metal workpiece, after which the following threads engage the hole wall and form internal threads. This allows drilling, tapping, and fastening to be completed in a single installation operation.
Whether a separate pilot hole can be omitted still depends on the workpiece material, thickness, hardness, and drilling capability of the screw.
Reduces the Need for Pre-Drilling
Compared with pointed or flat-point self-tapping screws, DRILL TAPPING screws can drill directly into suitable material thicknesses, reducing the need for a separate pilot-hole drilling process and helping shorten installation time.
May Eliminate the Need for a Separate Nut
The screw can form internal threads directly in the metal workpiece. In certain one-sided assembly applications or structures where a nut cannot be installed from the back side, this can reduce the need for nuts and other fastening components.
Improves On-Site Installation Efficiency
Installers do not need to frequently switch between drilling and fastening tools, helping reduce process changes, component positioning, and hole-alignment time. This makes DRILL TAPPING suitable for high-volume installation applications such as metal roofing, wall panels, HVAC ductwork, and light-gauge steel structures.
Drill-Point Design Improves Initial Engagement
The drill point helps position the screw and initiate cutting into the workpiece, reducing the tendency of conventional pointed screws to slip or wander on smooth metal surfaces.
Before installation, the workpiece surface, installation angle, and tool speed should still be confirmed to avoid misalignment.
Suitable for Joining Multiple Metal Layers
The drill point can penetrate overlapping metal sheets, after which the threads clamp the layers together. This makes DRILL TAPPING suitable for sheet-metal lap joints, metal profile fastening, and panel-to-frame assembly.
The total workpiece thickness must remain within the effective working range of the drill point and threads.
Multiple Drill-Point Lengths Available
Short, standard, or long drill points can be selected according to single-layer or multi-layer material thickness. The drill point should fully penetrate all workpieces before the threads begin to engage and tighten the assembly.
Multiple Head Types and Drive Options
Hex washer heads, pan heads, countersunk heads, and other head types can be selected according to product appearance, installation tools, available space, and torque requirements. Drive options can include external hex, Phillips, Torx, and others.
Can Be Used with Waterproof Sealing Washers
For roofing panels, exterior wall panels, and outdoor metal structures, DRILL TAPPING screws can be combined with metal washers and EPDM sealing washers. Compression around the screw head can help reduce the possibility of water entering through the mounting hole.
Actual waterproofing performance depends on washer material, compression amount, workpiece surface condition, and installation quality.
Suitable for Automated and High-Volume Fastening
DRILL TAPPING screws with consistent specifications can be used with feeding equipment, dedicated sockets, and automatic fastening systems, making them suitable for sheet metal, enclosures, appliances, and high-volume metal component production.
Multiple Materials and Surface Treatments Available
Depending on strength, drilling capability, corrosion resistance, weather resistance, and environmental requirements, carbon steel, alloy steel, or stainless steel can be selected together with various surface treatments.
Customization Based on Drawings and Samples
DRILL TAPPING screws can be customized according to customer engineering drawings or physical samples, including head type, drive style, thread diameter, thread pitch, length, drill-point type, drill-point length, material, hardness, tolerances, heat treatment, and surface treatment.
Common Applications
DRILL TAPPING screws are commonly used in:
- Metal roofing and corrugated sheet fastening
- Metal exterior wall panels and curtain-wall structures
- Light-gauge steel structures and steel profile assembly
- Sheet metal, enclosures, and cabinets
- HVAC ducts and ventilation equipment
- Solar mounting structures and metal accessories
- Electronic and electrical equipment
- Automotive and motorcycle sheet-metal components
- Home appliances and consumer products
- Metal furniture and display racks
- Doors, windows, and construction hardware
- Mass-production and automated fastening lines
Key Considerations When Selecting DRILL TAPPING
Before selection, confirm the workpiece material, hardness, single-layer and total thickness, drill-point length, effective thread engagement length, and expected load. A longer drill point is not necessarily better and should be selected according to actual material thickness and available assembly space.
The drill point must fully penetrate the workpiece before the threads begin normal engagement. If the threads contact the workpiece before the drill point has completely penetrated, the screw may spin without advancing, the drill point may break, the sheet layers may separate, or fastening may fail.
Appropriate rotational speed, downward force, and tool torque should be set during drilling. If the speed is too low, cutting may be inefficient. Excessive speed may cause overheating, dulling of the drill point, or damage to the surface treatment. Insufficient downward force may cause slipping, while excessive force may cause drill-point breakage.
The drilling capacity of the screw should exceed the total workpiece thickness, while the threaded section must still provide sufficient effective engagement length. If the sheet is too thin, the hole becomes oversized, or tightening torque is excessive, thread stripping or pull-through may occur.
The material and heat treatment of stainless steel self-drilling screws differ from those of conventional carbon steel products. Their actual drilling capability should therefore be confirmed according to the specific product specification rather than judged solely by appearance or material designation.
When a waterproof washer is used, the rubber element should not be over-compressed during tightening, as this may cause the washer to bulge outward, crack, or lose elasticity. Insufficient compression may also prevent a complete seal from forming.
For outdoor, coastal, humid, or corrosive environments, the screw material, surface treatment, weather resistance of the sealing washer, and the risk of galvanic corrosion between the screw and workpiece should also be evaluated.


