


Single-Start Thread for Easier Control During Fastening
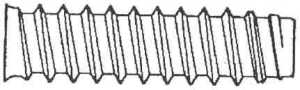
TYPE-B uses only one helical thread start, so its axial advance per revolution is relatively easy to control. This makes it suitable for assembly operations where driving depth, stopping position, and final clamping condition are important.
Easier Torque Control
Compared with faster-advancing twin-start screws, the slower axial advance of a single-start thread gives electric screwdrivers or automatic fastening equipment more time to react and stop, reducing the possibility of continued rotation after the screw head seats against the workpiece.
Actual torque control should still be verified according to tool speed, workpiece material, and shut-off settings.
Forms Internal Threads in the Workpiece
When driven into a properly sized pilot hole, TYPE-B can use its own threads to cut or displace the hole wall and form mating internal threads, reducing the need for a separate tapping operation.
Whether pre-drilling is required depends on the screw point design, workpiece material, thickness, and hardness.
May Eliminate the Need for a Separate Nut
TYPE-B can engage directly with the threads formed in the workpiece, making it suitable for one-sided assembly, structures where a rear-side nut cannot be installed, or products with limited internal working space.
Provides Stable Thread Engagement
The single-start thread forms a continuous and regular helix along the screw shank, allowing stable engagement with the workpiece hole wall. Selecting the proper thread diameter, thread pitch, and effective engagement depth helps maintain clamping force and pull-out strength.
Suitable for Precise Driving Depth
Because the axial advance is easier to control, TYPE-B is suitable for assemblies where the screw must not be driven too deeply, where blind-hole depth is limited, or where contact with internal components must be avoided.
For blind-hole applications, adequate clearance should still be provided between the screw point and the bottom of the hole.
Helps Reduce the Risk of Over-Tightening
At the same tool speed, the axial advance of a single-start thread is generally slower than that of a twin-start thread. This makes it easier for the operator or equipment to stop at the intended position, helping reduce the risk of plastic boss cracking, thread stripping in thin sheet metal, or excessive compression of the workpiece.
Suitable for Plastic Parts and Thin-Sheet Assembly
Thread pitch, thread depth, thread angle, and pilot hole size can be adjusted according to the workpiece material, allowing TYPE-B to be used with engineering plastics, general plastics, thin metal sheets, and die-cast components.
Because material hardness, toughness, and thickness vary significantly, actual fastening tests should be performed before mass production.
Simplifies Tapping and Assembly Processes
Once the specified hole is prepared, TYPE-B can form the internal thread and fasten the component in the same operation, reducing pre-tapping, nut installation, and multi-component assembly steps.
Suitable for Manual and Automated Fastening
TYPE-B can be installed with manual tools, electric screwdrivers, pneumatic tools, or automatic fastening equipment, making it suitable for maintenance work, small-batch production, and high-volume automated assembly lines.
Multiple Head and Point Designs Available
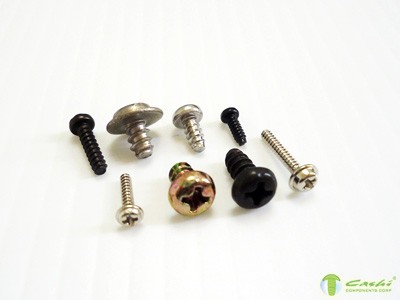
Depending on product appearance, installation tools, workpiece material, and fastening requirements, TYPE-B screws can be designed with pan heads, countersunk heads, hex heads, and other head types, together with pointed ends, flat ends, cutting points, pilot points, or other point structures.
Multiple Materials and Surface Treatments Available
Depending on strength, rust resistance, corrosion resistance, and operating environment, carbon steel, alloy steel, or stainless steel can be selected together with zinc plating, nickel plating, black oxide, phosphate coating, passivation, or other surface treatments.
Customization Based on Drawings and Samples
TYPE-B screws can be customized according to customer engineering drawings or physical samples, including screw head type, drive recess, thread diameter, thread pitch, single-start thread profile, overall length, point structure, material, hardness, tolerances, heat treatment, and surface treatment.
Common Applications
TYPE-B screws are commonly used in:
- Plastic housings and engineering plastic components
- Electronic and electrical equipment
- Home appliances and consumer products
- Automotive and motorcycle interior components
- Telecommunications and information equipment
- Thin metal sheets and sheet metal structures
- Aluminum alloy and zinc alloy die-cast parts
- Enclosures, cabinets, and control panels
- Furniture and wooden products
- Instruments and precision equipment
- One-sided assembly locations or areas where rear-side nut installation is difficult
- Assemblies requiring controlled driving depth
- Mass-production and automated fastening lines
Key Considerations When Selecting TYPE-B
Before selection, first confirm that “single thread” refers to a single-start thread rather than a single special tooth, a short threaded section, or another internal product designation. The actual thread profile, thread pitch, and lead should be confirmed according to the engineering drawing or physical sample.
Pilot hole size directly affects driving and fastening performance. If the pilot hole is too small, driving torque may become excessively high, potentially causing screw breakage, drive recess damage, or workpiece cracking. If the pilot hole is too large, thread engagement may be insufficient, resulting in free spinning, thread stripping, or reduced pull-out strength.
For plastic applications, the boss outside diameter, wall thickness, pilot hole depth, and material properties should be confirmed. An oversized screw diameter, excessive engagement depth, or excessive tightening torque may cause stress whitening, expansion, or cracking of the boss.
For metal and die-cast applications, the screw surface hardness must be sufficient to form threads in the workpiece while the core retains adequate toughness, helping reduce the risk of thread wear or brittle screw fracture.
Fastening tools should be set to appropriate rotational speed, downward force, and shut-off torque. Although a single-start thread makes driving position easier to control, excessive torque can still cause thread stripping, hole enlargement, or workpiece deformation.
TYPE-B screws are not intended for unlimited repeated assembly and disassembly. Repeated removal may wear the internal threads in the workpiece or enlarge the hole, reducing driving torque and pull-out strength during subsequent installations.
Before mass production, driving torque, tightening torque, stripping torque, failure torque, and pull-out strength should be tested to confirm that the selected thread profile, pilot hole, and fastening parameters provide an adequate process safety margin.


